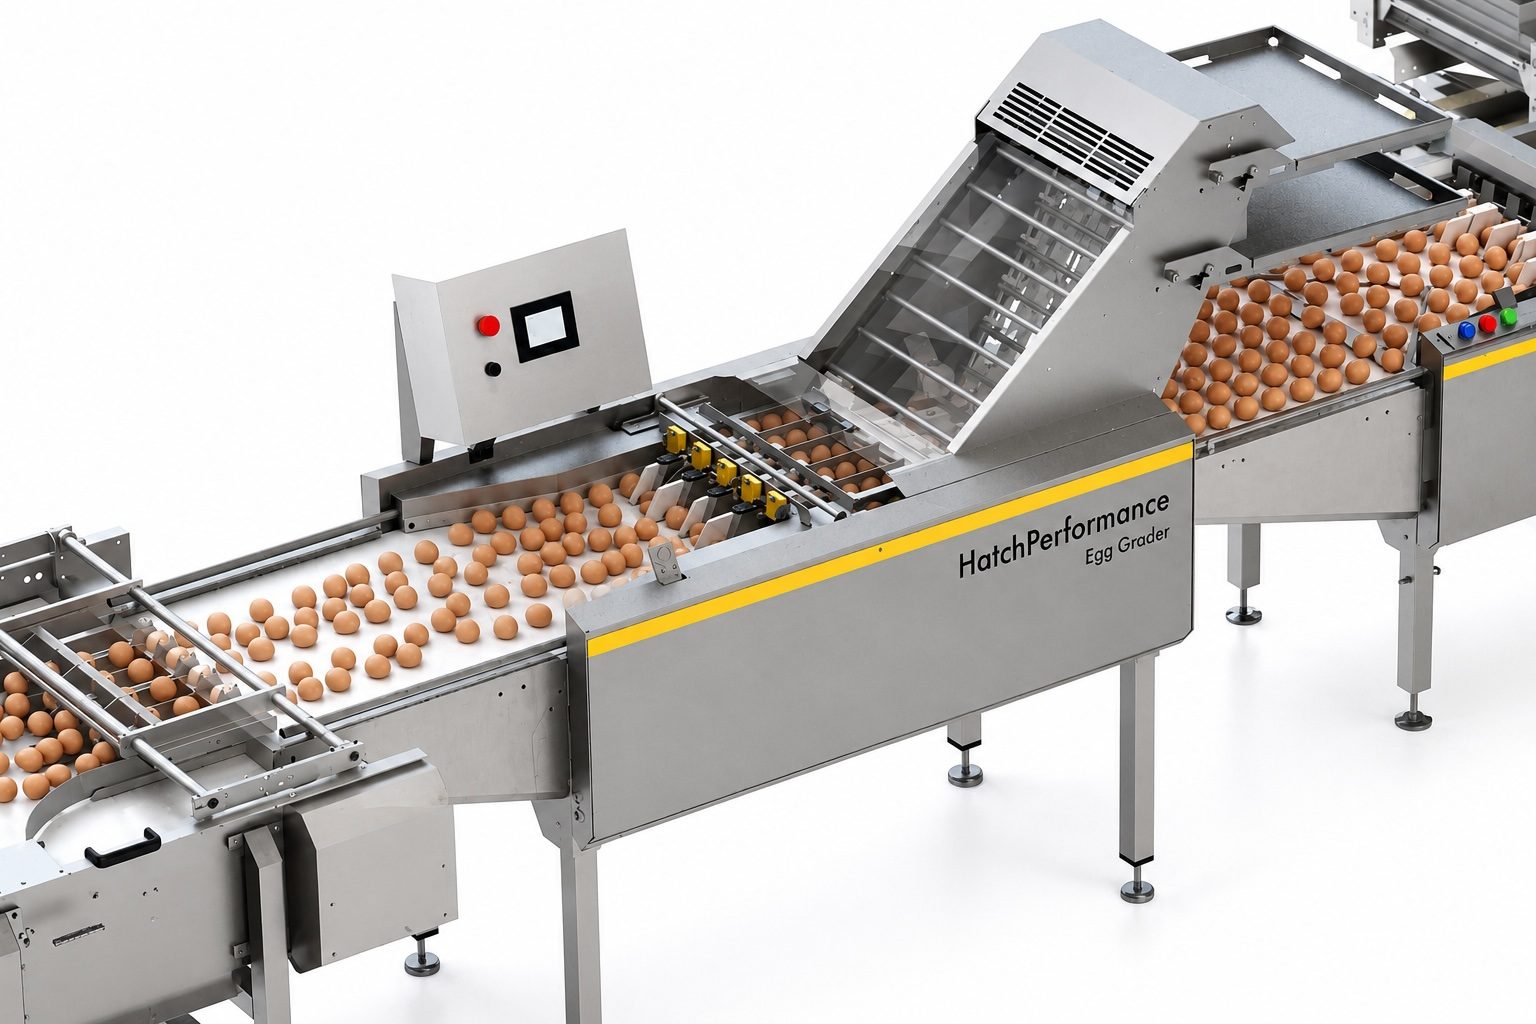
Before reaching our customers, every egg undergoes a comprehensive quality inspection using our HatchPerformance Egg Grader system.
Quality is the foundation of everything we do. Here's exactly what happens between the farm and your delivery.
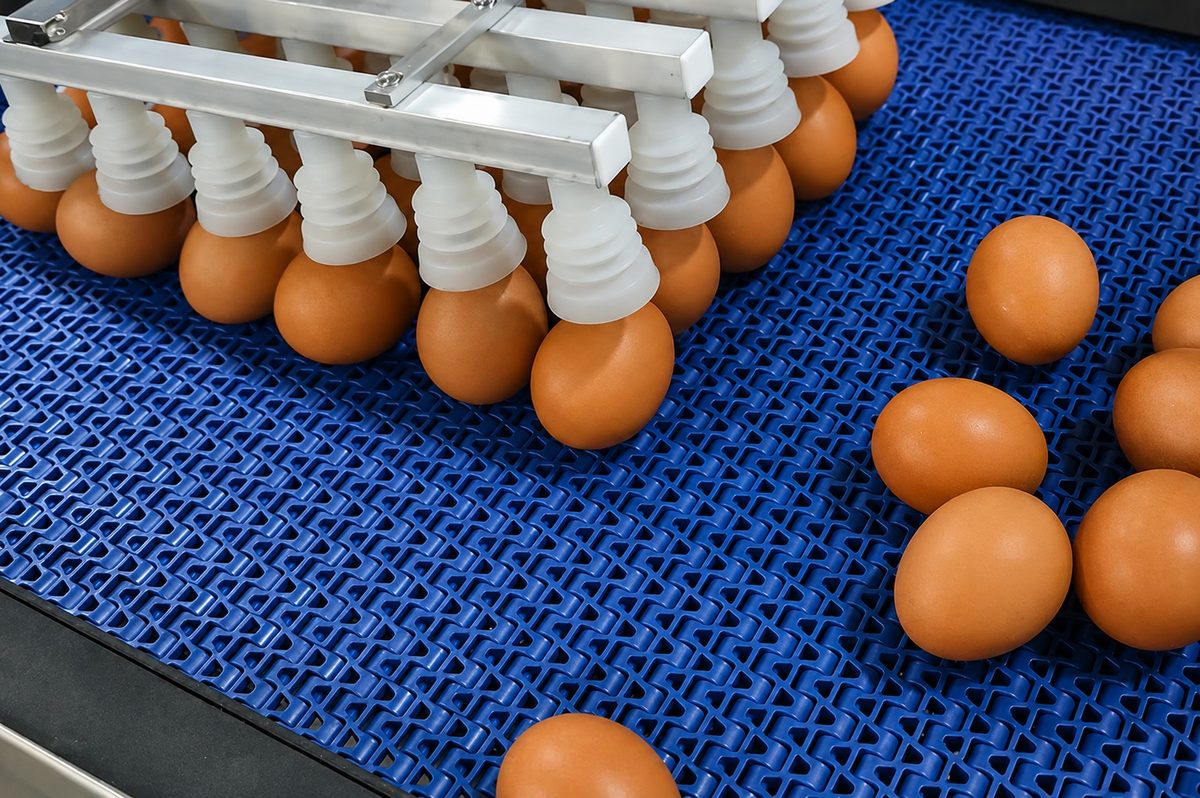
Fresh eggs are carefully placed onto an automated conveyor system — including a gentle vacuum-lifting mechanism that picks up to 30 eggs at a time — designed to minimize impact and reduce the risk of cracks.
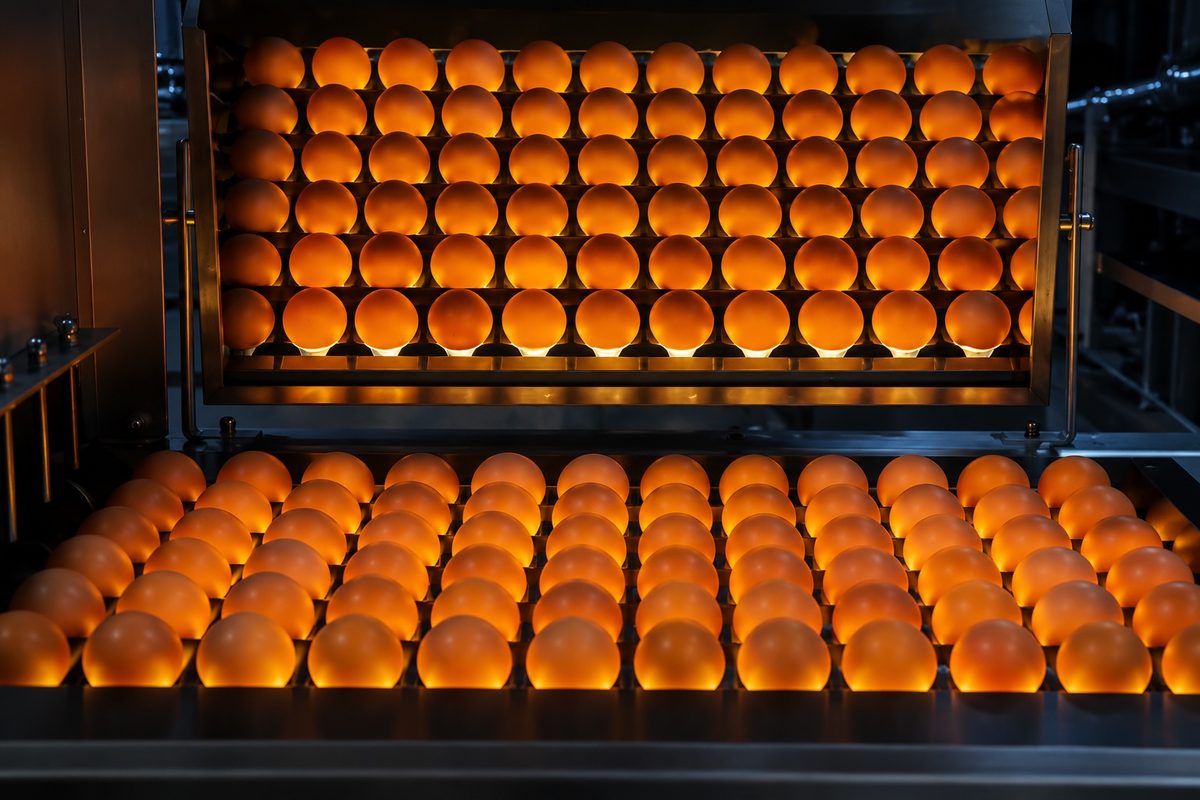
Each egg is candled and inspected for visible defects such as:
Eggs that fail inspection are removed from the production line.
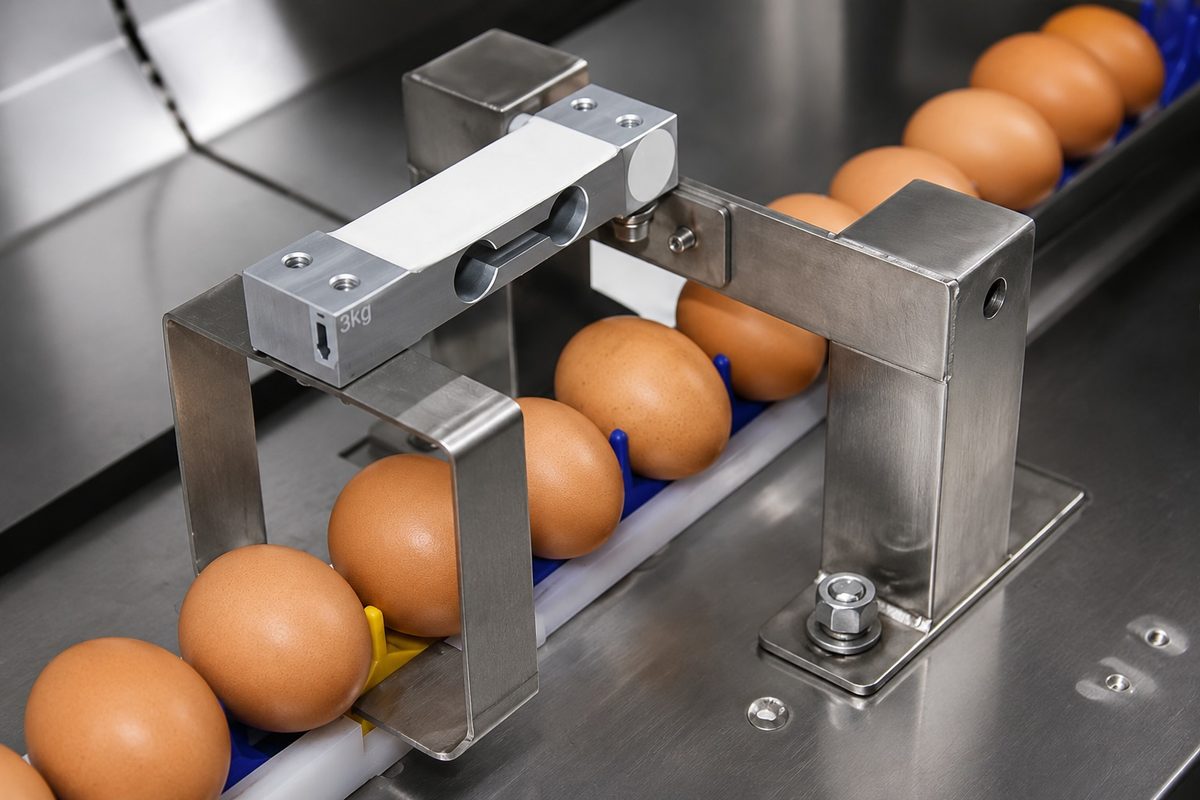
Every egg is weighed individually using high-precision electronic sensors. This guarantees accurate size classification, egg by egg, tray by tray.
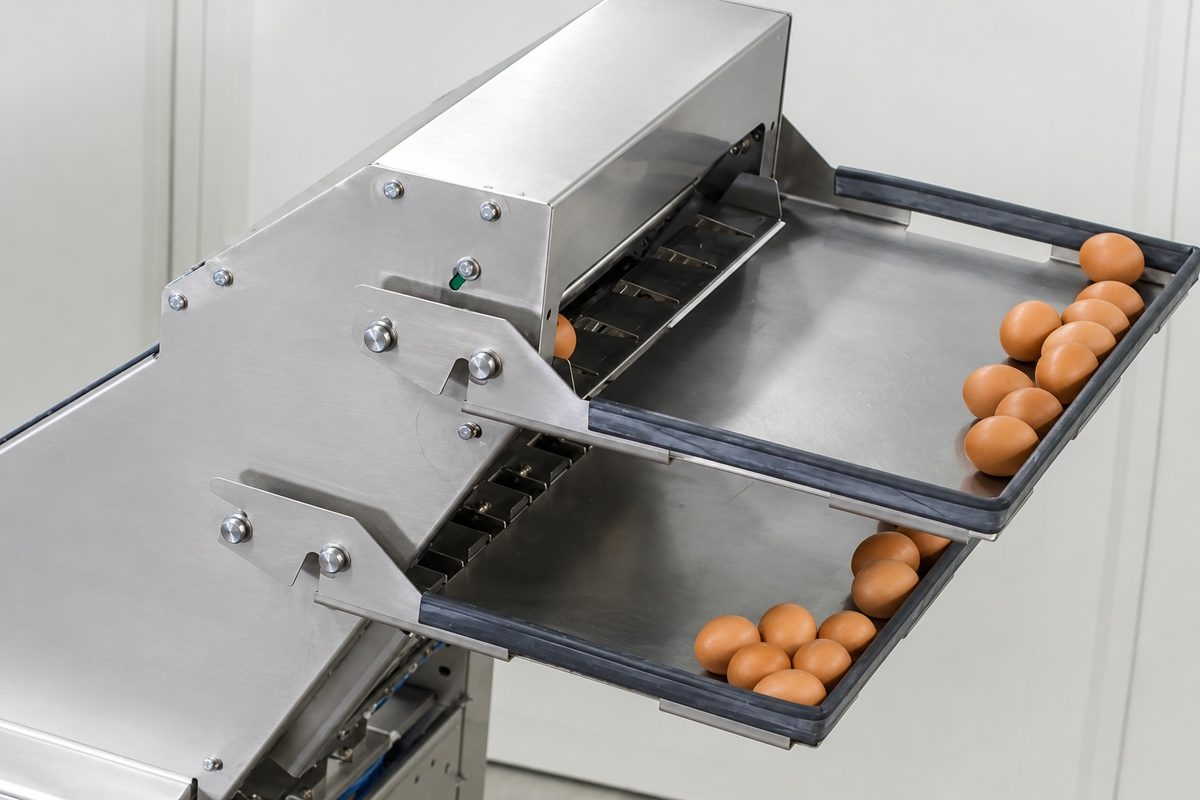
The machine sorts eggs into:
This ensures customers receive consistent products in every shipment.
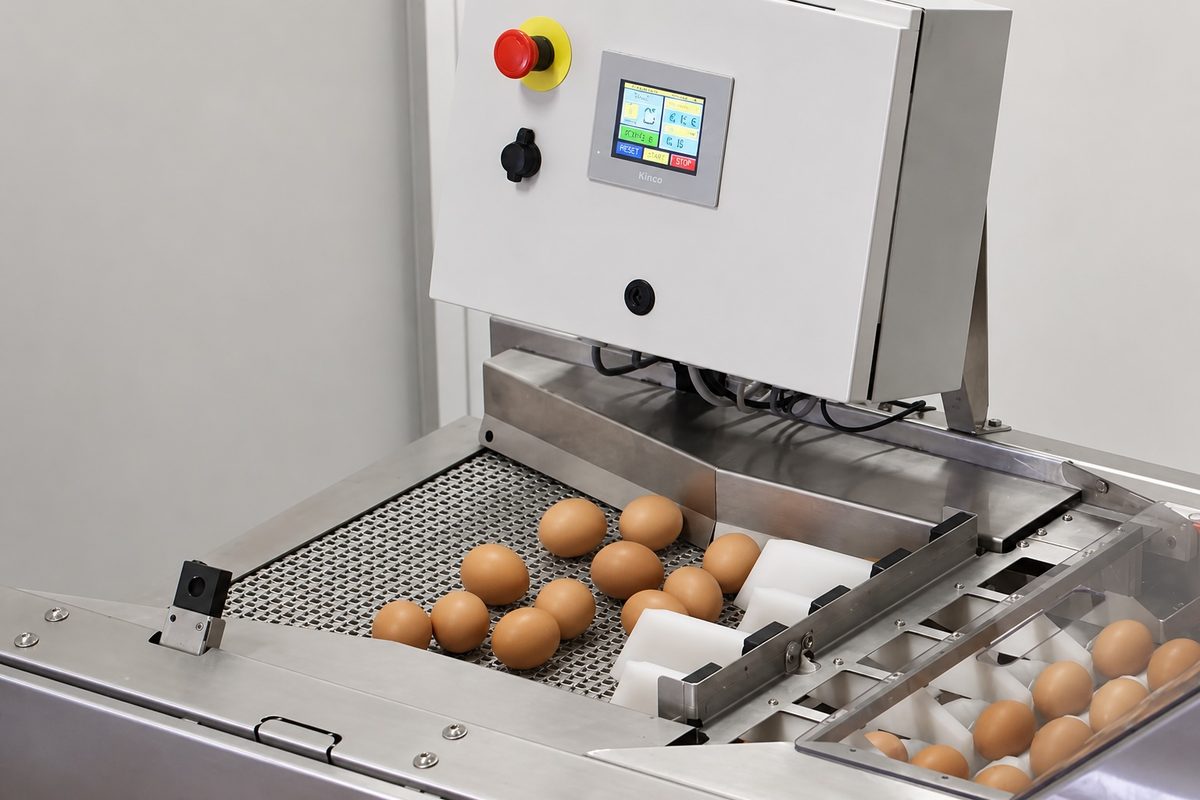
Our team monitors the grading system's control panel and performs additional quality checks before packaging.
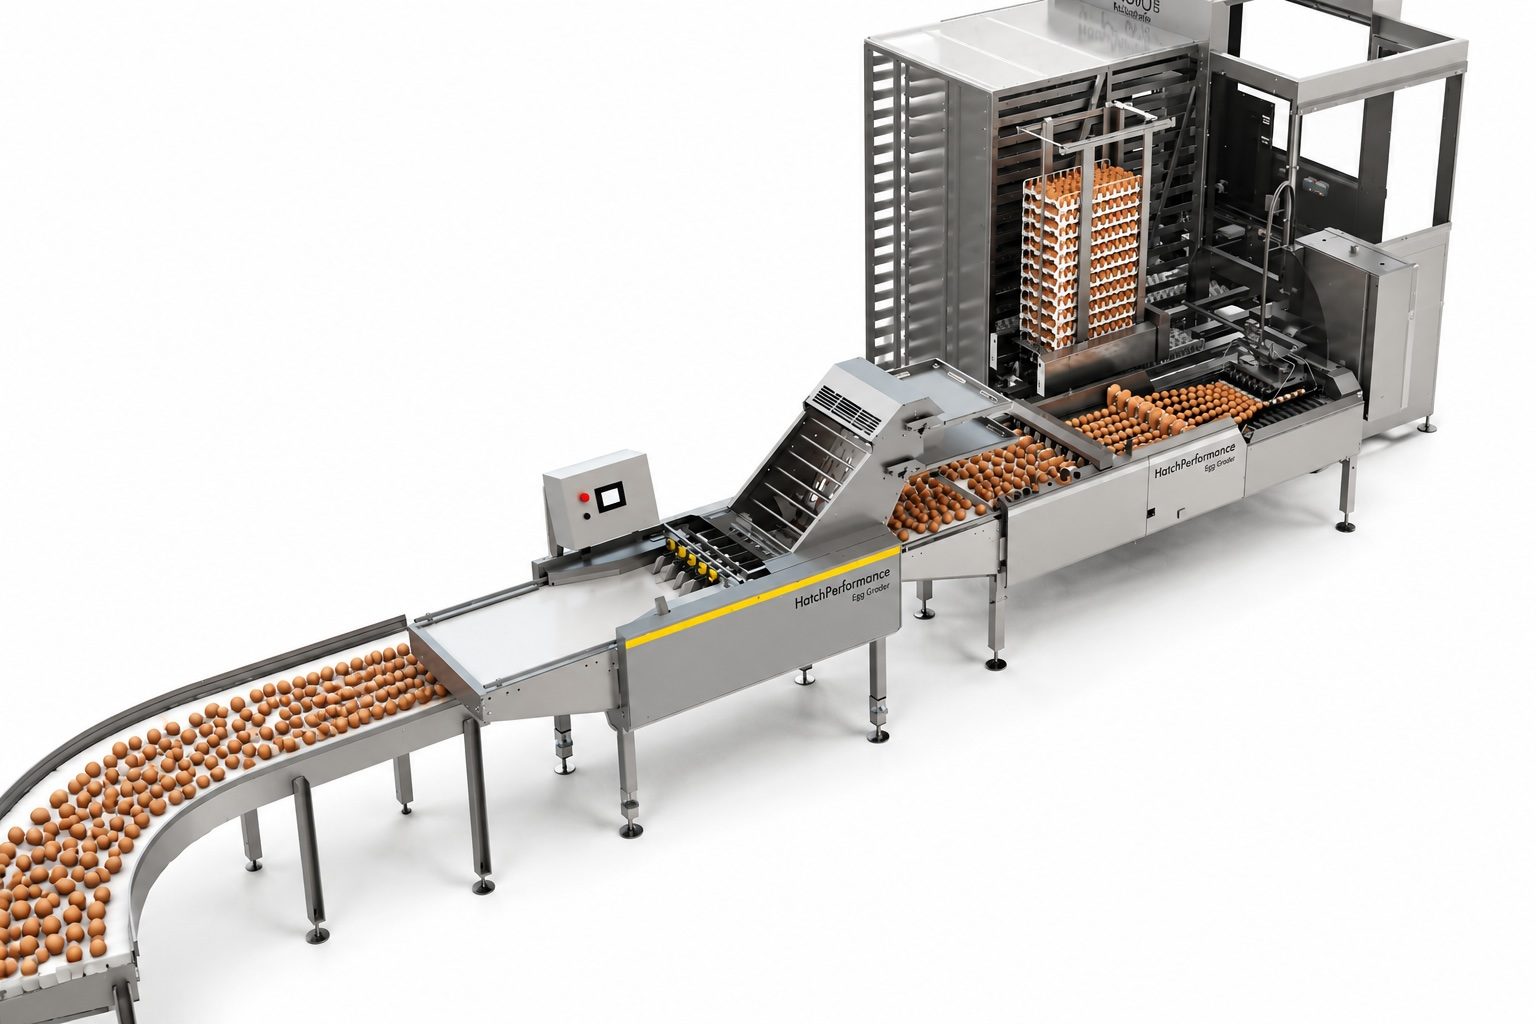
Eggs are carefully packed and prepared for transportation, ensuring freshness is maintained until delivery.
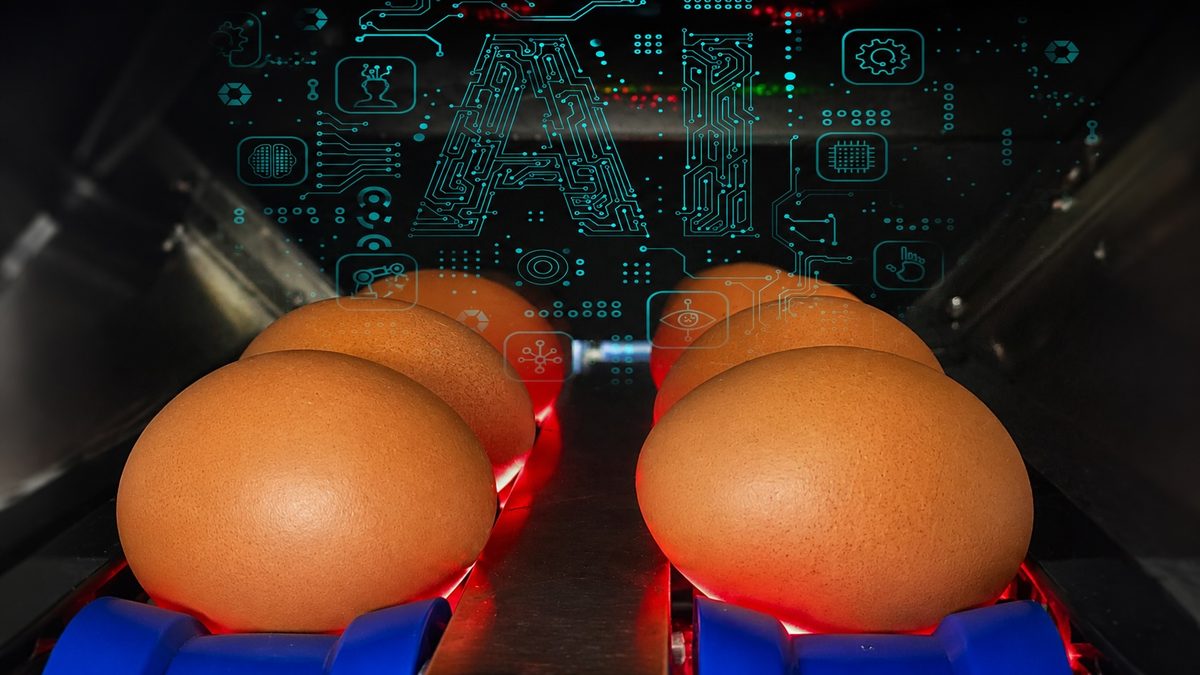
Alongside mechanical grading, our system uses visual inspection technology to catch defects that are easy for the human eye to miss — helping us remove damaged eggs earlier and keep the line moving efficiently.
The result is a faster, more consistent inspection process that protects both product quality and food safety, shipment after shipment.
Modern egg grading provides important advantages for businesses.
Essential for bakeries and food manufacturers where recipe accuracy matters.
Only eggs that meet our standards are delivered.
Damaged eggs are removed before packaging.
Accurate sorting minimizes rejected products.
Businesses receive products that consistently meet expectations.
See it for yourself — request a sample shipment or talk to our team about your business's requirements.